
 joyce@taisenfurniture.com
 0086 15356090777


What Defines a Reliable Hotel Furniture Supplier
Executing a large-scale hospitality project requires precision, capital, and a tightly synchronized supply chain. For properties scaling beyond 300 keys, procuring fixtures, furniture, and equipment (FF&E) represents a substantial portion of capital expenditure. Securing a manufacturing partner capable of delivering high-volume orders without compromising structural integrity or design intent is paramount for project success. To navigate this complex process, procurement teams must systematically evaluate suppliers across four critical stages: assessing manufacturing capability, verifying compliance, evaluating logistics, and making the final selection.
Supplier Reliability as a Project Risk Factor
In commercial hospitality development, supply chain volatility translates directly into financial exposure. A supplier’s inability to meet production milestones can delay an entire property opening. For a standard 300-key property, a delay in FF&E delivery can result in deferred revenue exceeding $30,000 per day—an illustrative figure that varies dramatically based on market Average Daily Rate (ADR), occupancy levels, and seasonality—alongside compounding holding costs and extended construction loan interest. Reliability, therefore, is not merely a metric of product quality, but a critical project risk-management variable that dictates the overall financial viability of the build. Strategic procurement must also account for macro-level risks, such as sole-source vulnerability and currency fluctuation exposure, which are critical reliability factors for large international FF&E programs.
Key Reliability Criteria for FF&E, Casegoods, and Seating
Distinct categories of assets require varying baseline reliability metrics. When sourcing hotel furniture, procurement teams must evaluate casegoods for veneer thickness (typically demanding a common benchmark of 0.6mm for commercial wear, though luxury and budget tiers often deviate) and core substrate stability. Seating must be evaluated against rigorous structural standards, such as BIFMA X5.4 for public lounge seating or relevant ASTM structural testing, rather than assuming standard office requirements apply universally. High-traffic hospitality seating typically requires weight capacities expected by industry rules of thumb to exceed 300 lbs, alongside foam density ratings of at least 2.5 to 3.0 lbs/cu.ft. as a general benchmark to prevent premature degradation. Standard 2.0 ratings are residential-grade and will not reliably deliver the expected 7-to-10-year commercial lifecycle. A reliable supplier demonstrates mastery across these distinct material categories, ensuring that a lounge chair and a built-in wardrobe both meet rigorous commercial expectations.
How to Assess Manufacturing Capability
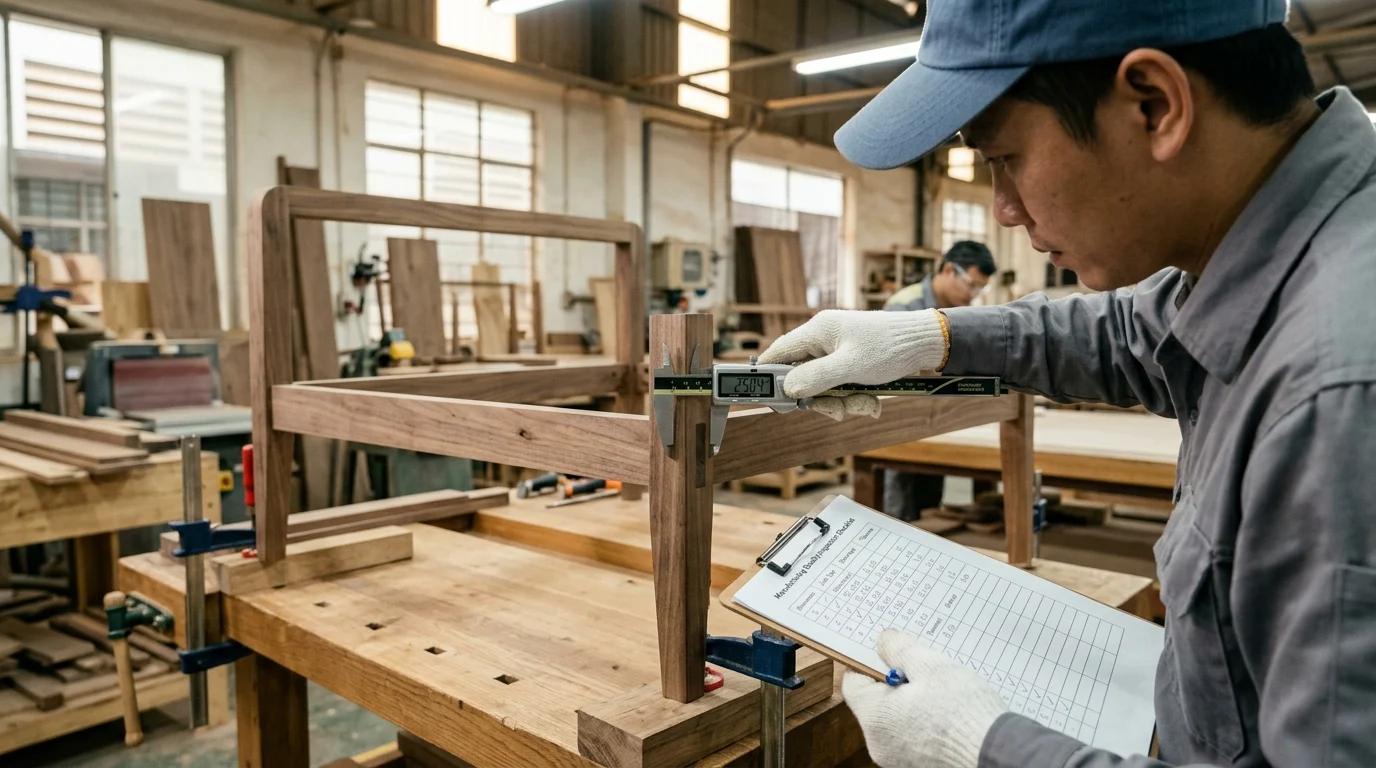
Evaluating a manufacturer’s true capabilities requires looking beyond marketing collateral and examining their operational infrastructure. A critical first step is verifying whether the supplier is a direct manufacturer or a trading company intermediary. Relying on undisclosed intermediaries introduces severe risks regarding quality control, accountability, and margin inflation. Procurement directors must validate that a factory possesses the physical footprint, machinery, and engineering acumen necessary to execute complex custom designs at scale.
Production Capacity and Engineering Expertise
A supplier’s throughput must align with the project’s critical path. For a 500-room resort, depending on the SKU mix and complexity, a factory might need to demonstrate a sustained production capacity of 1,500 to 2,000 casegood units per month as an illustrative benchmark. Furthermore, engineering expertise is critical during the shop drawing phase. The manufacturer must employ in-house CAD engineers who can translate conceptual architectural renderings into manufacturable blueprints, optimizing joint construction and hardware integration for high-traffic environments without inflating unit costs. When transmitting these proprietary CAD files overseas, establishing strict design IP protection and confidentiality protocols (such as robust NDAs) is essential to safeguard the project’s unique design assets.
Samples, Mock-Ups, Materials, and Finishes
The model room phase serves as the ultimate litmus test for a manufacturer’s capability. Reliable suppliers typically require 30 to 45 days to produce a first-off prototype or mock-up room. During this phase, project managers assess the accuracy of finish matching, the durability of specified textiles, and the precision of edge-banding. Tolerances for finish variations must be established early, utilizing universally recognized standards such as the Pantone Matching System or physical control samples signed and dated by the design firm.
Factory Capability Comparison Checklist
To objectively evaluate competing factories, procurement teams utilize standardized capability matrices. This ensures apples-to-apples comparisons regarding infrastructure, automation, and labor pools. Note that dollar-based output, facility size tiers, and freight benchmarks are primarily oriented toward offshore (often Asian) export manufacturing; domestic or near-shore suppliers may operate under vastly different scale and cost models. Therefore, the classifications below serve as illustrative baselines rather than absolute rules.
| Assessment Criteria | Tier 1 Factory (Ideal for 500+ Keys) | Tier 2 Factory (Suitable for <200 Keys) |
|---|---|---|
| Facility Size | > 25,000 sqm | 10,000 – 25,000 sqm |
| Monthly Output Capacity | $3M – $5M+ | < $1M |
| Automated CNC Machinery | 10+ multi-axis machines | 1 – 3 basic routing machines |
| In-House Engineering Team | 15+ dedicated CAD draftsmen | Outsourced or < 3 draftsmen |
| Material Sourcing | Direct global mill relationships | Local wholesale markets |
How to Verify Compliance and Quality Assurance
In the hospitality sector, aesthetic appeal is secondary to guest and occupant safety and regulatory adherence. Establishing rigorous quality assurance (QA) frameworks and verifying compliance with international safety standards protects the asset owner from liability and ensures the longevity of the investment.
Certifications, Fire Ratings, and Sustainability Standards
Hotel FF&E must comply with stringent localized fire and safety codes. Upholstered seating must typically meet the California Technical Bulletin 117-2013 (CAL 117-2013) or the UK’s BS 5852 standard for flammability in guest rooms, though hospitality public spaces often require stricter benchmarks such as CAL 133, NFPA 260/261, or ASTM E1537. Textiles are commonly expected to surpass a benchmark of 50,000 double rubs on the Wyzenbeek scale for high-traffic durability, though this can vary by property tier and specific application. Additionally, corporate ESG mandates increasingly require wood products to bear FSC (Forest Stewardship Council) certification and finishes to utilize low-VOC (Volatile Organic Compound) lacquers. Procurement must distinguish between content-based regulatory limits, such as SCAQMD Rule 1113 which restricts VOC content (often under 275 grams per liter depending on the specific category), and emissions-based certifications like Greenguard, which measure off-gassing in the finished product. Both strategies are critical for compliance.
Inspection Protocols and Defect Tolerance
Quality cannot be inspected into a product; it must be engineered. However, robust inspection protocols remain the last line of defense. Industry-standard procurement relies on the Acceptable Quality Limit (AQL) methodology. For luxury hotel projects, third-party auditors typically enforce an AQL of 1.5 for major defects (e.g., structural instability, deep scratches) and 4.0 for minor defects (e.g., slight finish discrepancies on non-visible surfaces). Suppliers must agree to these thresholds in writing, absorbing the cost of rework for any batch that exceeds the permissible defect rate.
Required Documentation Before Purchase Orders
Before any capital is deployed via a Purchase Order (PO), a comprehensive documentation package must be finalized. This includes approved shop drawings, a detailed Bill of Materials (BOM) specifying hardware brands (e.g., Blum or Hafele hinges meeting industry rules of thumb for 80,000-cycle durability), and a finalized finishing schedule. The absence of granular documentation at this stage is a primary indicator of future quality fade.
How to Evaluate Logistics and Installation Support
Manufacturing the furniture is only half the battle; delivering it to a constrained construction site in sequence with the general contractor’s schedule requires exceptional logistical orchestration. A supplier’s ability to manage freight, customs, phased site deliveries, and on-site assembly is a critical differentiator.
Lead Times, Phased Deliveries, Warehousing, and Site Coordination
Global supply chains remain susceptible to disruption. Standard ocean freight from primary Asian manufacturing hubs to North American or European ports requires 35 to 45 days in transit, plus an additional 7 to 14 days for customs clearance and drayage. Reliable suppliers integrate a 14-day buffer into their lead times and offer phased delivery schedules. Beyond freight and warehousing, comprehensive installation support is vital. This includes coordinating white-glove delivery, deploying on-site assembly crews, and sequencing the unpacking and placement directly with the general contractor to minimize site disruption. This prevents site congestion, ensuring that floors one through five receive their casegoods only after drywall and painting are complete, while subsequent floors remain safely in climate-controlled warehousing.
Communication Cadence and Reporting Tools
Information asymmetry during the production and shipping phases creates severe operational bottlenecks. Top-tier suppliers utilize cloud-based reporting tools to provide weekly Work in Progress (WIP) updates. These reports should include photographic evidence of raw material staging, assembly line progress, and packaging. Once containers are sealed, the cadence shifts to real-time EDI (Electronic Data Interchange) tracking of ocean vessels and terminal discharge statuses.
How to Choose the Best Hotel Furniture Supplier
The final selection of a manufacturing partner must transcend basic unit pricing by synthesizing the insights gathered during the capability, compliance, and logistics evaluations. An analytical approach to procurement mitigates downstream risks and aligns the entire supply chain with the asset owner’s strategic objectives.
Total Cost Beyond Unit Price
Price-focused procurement focuses on the FOB (Free on Board) unit price, while expert procurement calculates the Total Landed Cost. The unit cost of a nightstand may appear 15% cheaper at Factory A, but once factoring in ocean freight, import duties (which can range from 0% to 25% depending on trade tariffs and origin), inland drayage, currency fluctuation exposure, and the cost of capital tied up in longer payment terms, the actual landed cost delta can swing by 25% to 40%. Structuring secure payment terms, such as utilizing Letters of Credit (LCs) rather than large uncollateralized wire transfers, is a critical risk-management element for large international programs. Reliable suppliers assist in value-engineering the product to optimize packaging dimensions, thereby reducing the total freight burden.
Decision Matrix for Capability, Compliance, and Service
To eliminate bias, procurement teams should deploy a weighted decision matrix. This quantifiable approach assigns numerical values to various supplier attributes based on project-specific priorities. The 30/25/25/20 weightings shown below are illustrative examples and should be recalibrated per project; for instance, fast-track builds may require a higher logistics weighting.
| Evaluation Category | Weighting | Key Metric Evaluated | Minimum Acceptable Standard |
|---|---|---|---|
| Unit & Landed Cost | 30% | Total cost delivered to site | Within 5% of project budget |
| Manufacturing Capacity | 25% | Monthly output vs. project schedule | 1.5x required monthly volume |
| Quality & Compliance | 25% | AQL history and ISO/FSC certifications | AQL 1.5 Major / CAL 117-2013 |
| Logistics & Service | 20% | Communication tools and freight management | Weekly WIP reports, DDP options |
Final Due Diligence Signals
Before countersigning the final contract, all prior evaluations must culminate in a final due diligence review. Rather than introducing new hurdles, this stage confirms the supplier’s overall reliability and synthesizes earlier findings. Pulling commercial credit reports (such as Dun & Bradstreet) verifies that the factory possesses the financial liquidity to execute the capacity claims evaluated earlier, ensuring they can procure raw materials for a multi-million-dollar order without demanding excessive upfront deposits. Evaluating sole-source vulnerability confirms that the logistics and supply chain frameworks are resilient enough to handle disruptions. Furthermore, commercial warranty terms, replacement-part availability, and after-sales service act as the final guarantees of the quality and compliance standards previously established. Finally, checking references strictly against properties of similar scale.
Steps from Supplier Shortlist to Final Selection
Transitioning from a shortlist of viable factories to a finalized partnership requires a structured approach that heavily stress-tests a supplier’s logistical and operational acumen. The process begins with a Request for Quotation (RFQ), advances to factory audits and model room reviews, and culminates in a logistical evaluation. Procurement managers must demand a mock shipping schedule during the RFP phase to evaluate the supplier’s understanding of container optimization—aiming for an optimal volumetric fill rate (often targeted around 85%, though this varies significantly by SKU mix and shipping lane) to minimize landed freight costs.
Key Takeaways
- Treat hotel furniture supplier reliability as a project risk factor because FF&E delays can defer opening revenue and increase financing or holding costs.
- Verify whether the supplier is a direct manufacturer, since undisclosed intermediaries can weaken accountability, quality control, and cost transparency.
- Match production capacity to the project schedule, especially for large resorts that may require 1,500 to 2,000 casegood units per month depending on SKU complexity.
- Evaluate casegoods and seating with category-specific standards, including commercial veneer benchmarks, substrate stability, structural testing, and foam density requirements.
- Specify hospitality-grade seating with durability targets such as 300-lb-plus weight capacity and 2.5 to 3.0 lbs/cu.ft. foam density where appropriate.
- Assess logistics, compliance, and macro risks such as sole-source exposure and currency fluctuation before making the final supplier selection.
Frequently Asked Questions
Why is supplier reliability critical in large hotel projects?
For properties above 300 keys, FF&E delays can postpone opening and create major revenue losses. Even one late furniture shipment can affect installation schedules, financing costs, and guest-ready deadlines.
What should procurement teams verify before choosing a hotel furniture supplier?
Teams should confirm manufacturing capacity, quality control systems, compliance documentation, material standards, logistics capability, and whether the supplier is a direct factory or an intermediary.
How can buyers assess a supplier’s production capacity?
Buyers should review factory size, machinery, staffing, monthly output, engineering support, and recent project history. For a 500-room resort, capacity may need to reach 1,500 to 2,000 casegood units per month.
What material standards matter for hotel casegoods?
Commercial casegoods should use stable substrates, durable finishes, and suitable veneer thickness. A 0.6mm veneer is often used as a benchmark for commercial wear, though requirements vary by brand tier.
What makes hospitality seating different from residential seating?
Hotel seating must withstand heavy daily use, often requiring structural testing such as BIFMA X5.4 or relevant ASTM standards, weight capacities above 300 lbs, and foam density around 2.5 to 3.0 lbs/cu.ft.
Post time: Sep-14-2026